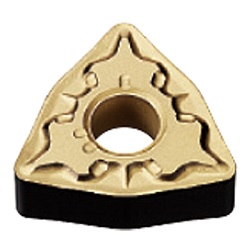
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin
M grade insert (with SH breaker) WNMG-SH.[Features]・80° equilateral unequal hexagon, negative insert, with hole・M-class double-sided chip breaker・Low depth of cut in the light cutting area・Ideal for high feed areas・Smooth chip discharge is possible with the curved cutting edge・Recommended for work material hardness 160-250HB・NX2525 for stable cutting of steel, stainless steel and cast iron (guideline for cutting conditions)・MC6115 and UE6105 for stable cutting of steel ( guideline for cuttin